China has long been a global leader in manufacturing, and the food packaging industry is no exception. Chinese food packaging manufacturers continue to set the standard for quality, innovation, and efficiency. This article delves into the top 10 Chinese food packaging manufacturers, highlighting their unique strengths, contributions to the industry, and the benefits they offer to businesses worldwide.



RFQ and Quality-Control Checklist
- Food type, dimensions, weight and filling temperature
- Direct-contact condition and required barrier
- Internal size, material, structure and closure
- Printing, finishes, quantity and destination
- Check dimensions, seals, glue, odor and migration documentation
- Test stacking, leakage, grease, moisture and transport performance
Printing and Premium Finishes
Define ink system, coating, window film, foil, embossing and acceptable color tolerance. Keep decorative finishes away from direct-contact and sealing areas unless specifically validated.
Inserts, Liners and Barrier Materials
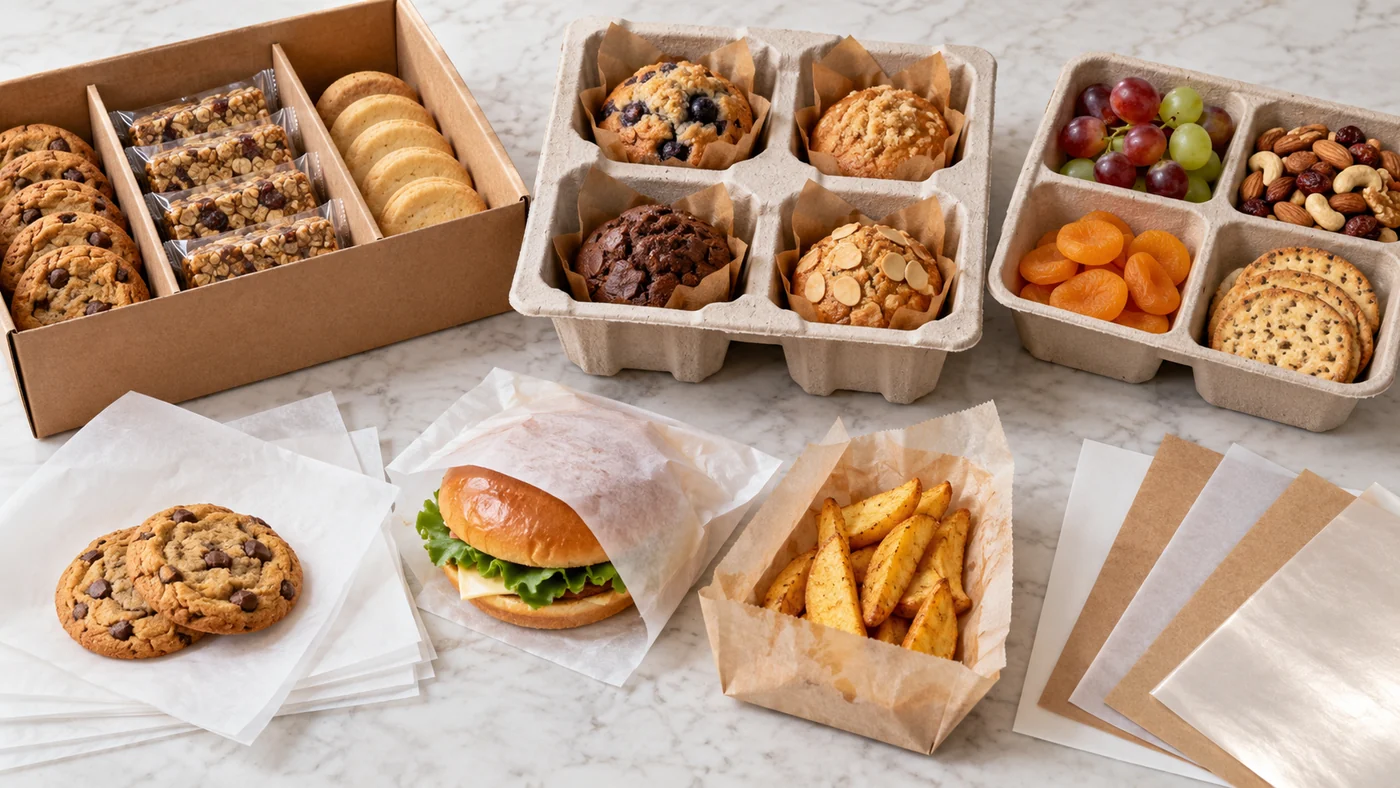
Specify grease, moisture, oxygen or aroma barriers according to the actual food. Confirm whether coatings, trays and liners touch food directly and request documentation for the destination market.
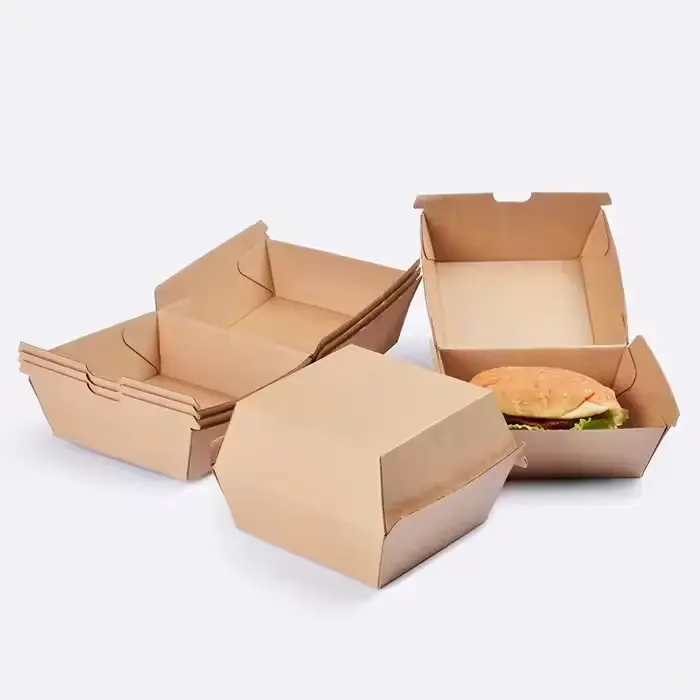
Takeout and Delivery Structure
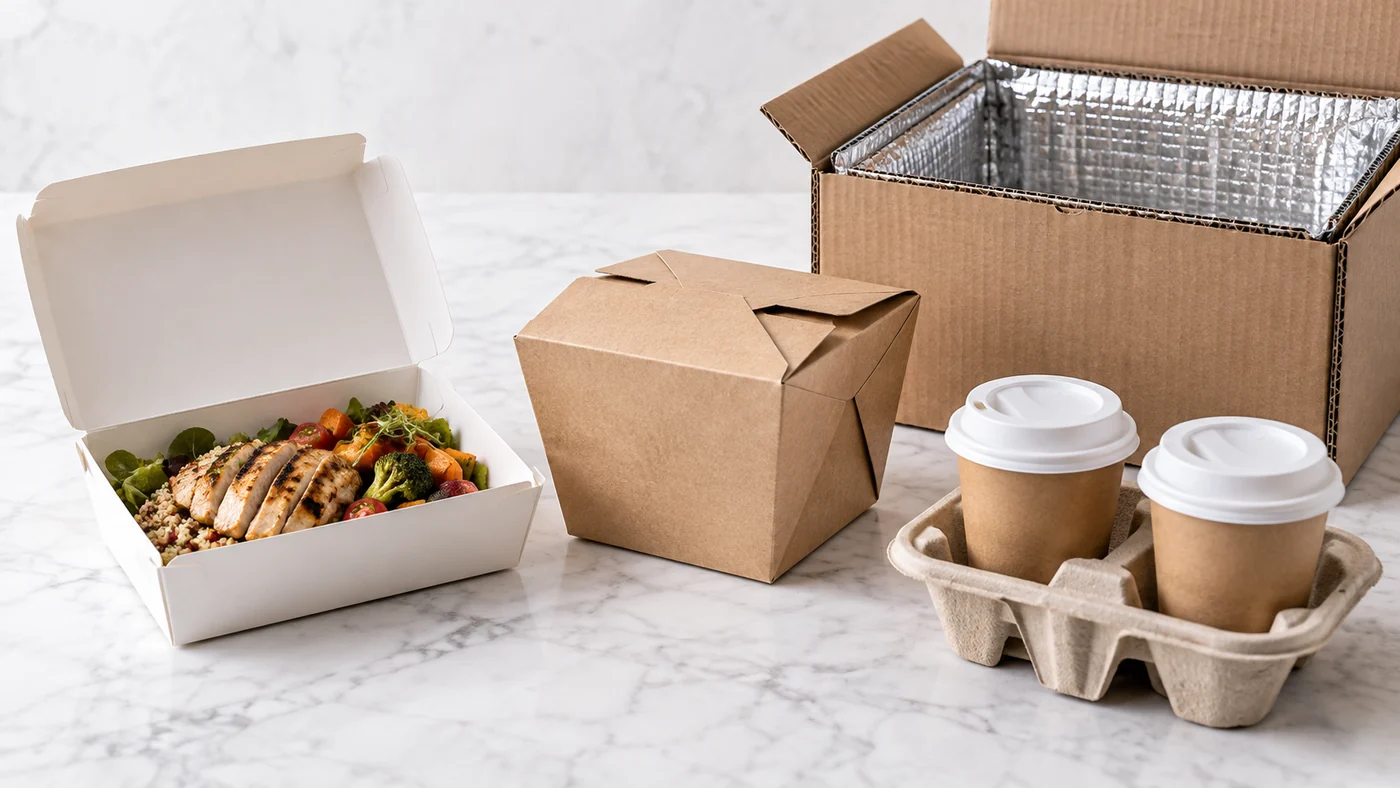
Check closure security, leak resistance, ventilation, stacking and temperature exposure. A retail food carton and an insulated delivery pack require different materials and testing.
Quick Answer: Choosing a Food Packaging Manufacturer in China
Select a supplier by matching the packaging format, food-contact condition, barrier requirement, filling temperature and distribution route. Provide product dimensions, weight, shelf-life needs, direct-contact details, material, printing, quantity per design, destination and required compliance documents. Approve a production-representative sample before mass production.

Food Packaging Formats and Product Links
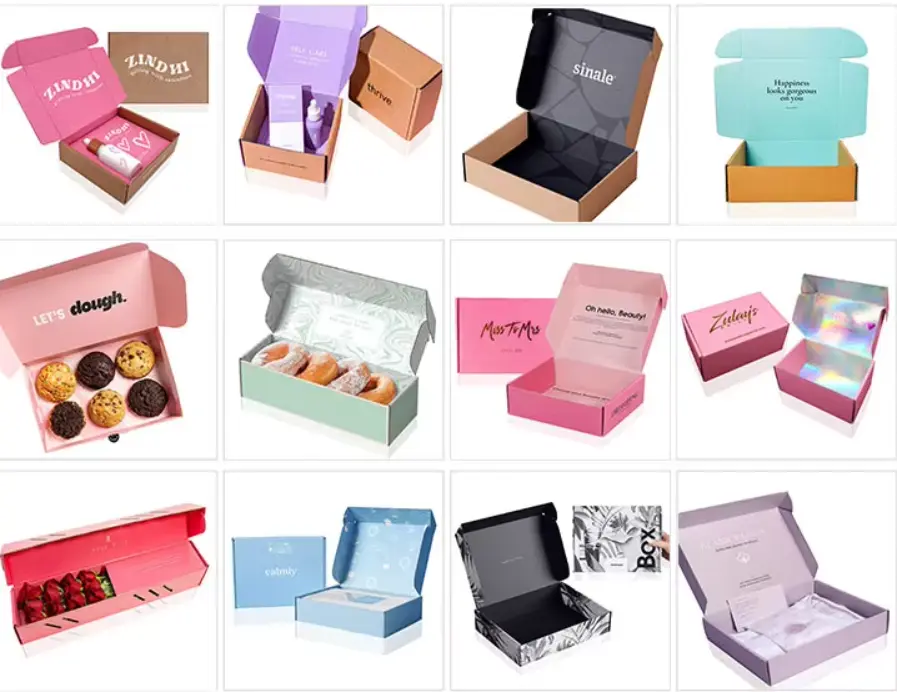
Pakoro supplies custom food packaging, folding cartons, paper carton boxes and corrugated mailer boxes. Choose paperboard cartons for retail presentation, corrugated structures for delivery protection, and documented liners or trays where direct food contact is involved.
Top 10 Food Packaging Manufacturers In China
| Position | Company | Established | Location | Employee Size |
| 1 | Pakoro | 2005 | Shenzhen, China | 100-150 |
| 2 | China National Packaging Corporation (CNPACK) | 1982 | Shandong, China | 13,300 |
| 3 | Zijiang Enterprise | 1993 | Fujian, China | 11,215 |
| 4 | Sihui Fujiwara Printing and Packaging Machinery Co., Ltd. | 1994 | Sihui, China | 6,290 |
| 5 | Shanghai Custom Packaging Co., Ltd. | 1997 | Shanghai, China | 4,262 |
| 6 | Guangzhou Packbest Air Packaging Co., Ltd. | 2000 | Guangzhou, China | 6,049 |
| 7 | Shantou Weiyi Packaging Co., Ltd. | 1996 | Shantou | 8,679 |
| 8 | Zhejiang Zhongxin Packaging Co., Ltd. | 2000 | Zhejiang, China | 4,170 |
| 9 | Shenzhen Prince New Material Co., Ltd. | 2009 | Shenzhen, China | 150+ |
| 10 | Foshan Nanhai Zhongnan Aluminum Wheel Co., Ltd. | 2008 | Foshan, China | 150+ |
1. Pakoro
Innovating for a Sustainable Future
Pakoro is a globally recognized name in packaging, and its Chinese division is no less impressive. With a strong focus on sustainability, Pakoro China develops eco-friendly packaging solutions that minimize environmental impact. Their products range from flexible and rigid packaging to specialty cartons, all designed to preserve food quality and extend shelf life.

Key Benefits
- Advanced sustainable materials
- Customizable packaging solutions
- High barrier properties for better food preservation
2. China National Packaging Corporation (CNPACK)
Industry Giant with a Comprehensive Portfolio
CNPACK is one of the largest packaging companies in China, offering a wide array of food packaging solutions. Their extensive portfolio includes flexible packaging, paper packaging, and rigid containers. Known for their rigorous quality control and innovative designs, CNPACK serves various industries, ensuring that their products meet the highest standards of safety and functionality.

Key Benefits
- Diverse product range
- Stringent quality assurance
- Innovative design capabilities
3. Zijiang Enterprise
Pioneering High-Performance Packaging
Zijiang Enterprise is renowned for its high-performance packaging solutions, particularly in the food and beverage sectors. Their state-of-the-art facilities and investment in research and development enable them to produce packaging that is both aesthetically pleasing and functionally superior.
Key Benefits
- High-quality materials and production processes
- Strong R&D focus
- Tailored solutions for food and beverage packaging
4. Sihui Fujiwara Printing and Packaging Machinery Co., Ltd.
Excellence in Printing and Packaging Machinery
Sihui Fujiwara specializes in the manufacturing of high-quality printing and packaging machinery, making them a critical player in the food packaging industry. Their machines are known for precision, efficiency, and reliability, helping food manufacturers maintain high standards of packaging.
Key Benefits
- Cutting-edge machinery
- High precision and efficiency
- Strong customer support and service
5. Shanghai Custom Packaging Co., Ltd.
Customized Solutions for Diverse Needs
Shanghai Custom Packaging Co., Ltd. stands out for its bespoke packaging solutions tailored to meet specific customer needs. Their focus on customization allows them to cater to a wide range of food products, ensuring optimal protection and presentation.

Key Benefits
- Extensive customization options
- High-quality printing and finishing
- Versatile packaging solutions


6. Guangzhou Packbest Air Packaging Co., Ltd.
Leading in Protective Packaging
Packbest specializes in air packaging solutions, providing innovative products that protect food items during transit. Their inflatable packaging is designed to reduce damage, ensuring that food reaches consumers in perfect condition.

Key Benefits
- Superior protective packaging
- Cost-effective solutions
- Environmentally friendly options
7. Shantou Weiyi Packaging Co., Ltd.
Expertise in Flexible Packaging
Shantou Weiyi Packaging Co., Ltd. is a leader in flexible packaging, offering a wide range of pouches, bags, and films for the food industry. Their products are known for their durability, high barrier properties, and excellent printability.

Key Benefits
- Durable and high-quality materials
- Excellent barrier properties
- Customizable printing options
8. Zhejiang Zhongxin Packaging Co., Ltd.
Commitment to Quality and Innovation
Zhejiang Zhongxin Packaging Co., Ltd. has made a name for itself through its commitment to quality and continuous innovation. They offer a comprehensive range of packaging solutions, including biodegradable and eco-friendly options, to meet the evolving needs of the food industry.

Key Benefits
- High-quality and innovative products
- Eco-friendly packaging options
- Comprehensive customer support
9. Shenzhen Prince New Material Co., Ltd.
Advanced Materials for Enhanced Packaging
Shenzhen Prince New Material Co., Ltd. specializes in advanced packaging materials that enhance food safety and shelf life. Their products are designed to withstand various environmental conditions, making them ideal for both local and international markets.
Key Benefits
- Advanced material technology
- Enhanced food safety and shelf life
- Suitable for diverse environmental conditions
10. Foshan Nanhai Zhongnan Aluminum Wheel Co., Ltd.
Versatility in Packaging Solutions
While primarily known for its aluminum products, Zhongnan Aluminum Wheel Co., Ltd. has diversified into food packaging with impressive results. Their aluminum-based packaging solutions offer superior protection and sustainability, making them a preferred choice for many food manufacturers.
Key Benefits
- High-quality aluminum packaging
- Strong protection and durability
- Sustainable and recyclable options
3 Qualities of the Best Food Packaging Manufacturer
Choosing the right food packaging manufacturer is crucial for businesses looking to ensure the safety, quality, and appeal of their products. The best food packaging manufacturers stand out due to their commitment to innovation, quality, and sustainability. Here are three key qualities that distinguish top-tier food packaging manufacturers:
1. Innovation and Technology
Cutting-Edge Solutions
Leading food packaging manufacturers invest heavily in research and development to stay ahead of industry trends and consumer demands. They leverage the latest technologies to create innovative packaging solutions that enhance product safety, extend shelf life, and improve user convenience. For instance, advancements such as smart packaging, which can monitor freshness or temperature, are a testament to the innovative capabilities of top manufacturers.
Customization Capabilities
The ability to offer customized packaging solutions tailored to the unique needs of different products and brands is a significant advantage. Top manufacturers provide a range of customizable options, including materials, shapes, sizes, and printing designs, ensuring that the packaging not only protects the food but also enhances its marketability.
2. Quality Assurance and Safety Standards
Rigorous Quality Control
High-quality food packaging is essential for preserving the integrity and safety of food products. The best manufacturers implement stringent quality control processes at every stage of production. This includes the use of high-quality, food-grade materials and adherence to international safety standards and certifications such as ISO, FDA, and BRC.
Reliable Supply Chain Management
Top manufacturers maintain robust supply chain management to ensure consistent quality and timely delivery. They work with reliable suppliers and employ advanced logistics solutions to manage production schedules and inventory efficiently. This reliability ensures that businesses can depend on them for consistent supply and quality.
3. Commitment to Sustainability
Eco-Friendly Materials
Sustainability is a growing concern in the food packaging industry, and the best manufacturers are at the forefront of this movement. They develop and utilize eco-friendly materials such as biodegradable plastics, recycled paper, and compostable films. By reducing the environmental impact of their packaging solutions, these manufacturers contribute to a more sustainable future.
Sustainable Practices
In addition to using sustainable materials, top manufacturers adopt environmentally responsible practices throughout their operations. This includes minimizing waste, reducing energy consumption, and implementing recycling programs. Their commitment to sustainability often extends to helping their clients achieve their own environmental goals by providing eco-friendly packaging options.

Conclusion
The Chinese food packaging industry in 2024 is characterized by innovation, quality, and a strong commitment to sustainability. These top 10 manufacturers exemplify the best of what the industry has to offer, providing businesses worldwide with cutting-edge packaging solutions that enhance food safety, extend shelf life, and meet diverse consumer needs. As the demand for high-quality food packaging continues to grow, these companies are well-positioned to lead the way, ensuring that their products not only meet but exceed industry standards.
Frequently Asked Questions
What should be included in a food packaging RFQ?
Include food type, dimensions, contact conditions, barrier needs, structure, materials, printing, quantity, destination and required documents.
Can printed paperboard touch food directly?
Do not assume it can. Define the contact condition and use documented food-contact materials, liners or trays.
How should takeout packaging be tested?
Test closure, leakage, grease, moisture, heat, stacking and transport with the actual food.
Which packaging is suitable for delivery?
Corrugated delivery packs with suitable cushioning or thermal components are often used, depending on product and route.
What barrier does food packaging need?
The required grease, moisture, oxygen or aroma barrier depends on the food and shelf-life target.
How are food packaging colors approved?
Use an agreed proof or production sample on the specified substrate and finish.
What quality checks are important?
Check dimensions, material, glue, seals, odor, print, barcode and packed-product performance.
What is a typical MOQ?
MOQ varies by format and printing; Pakoro generally focuses on custom quantities from about 500 units.